
HIGH-SPEED PRODUCTION LINE AUTOMATION
High-Speed End-of-Line Automation for Continuous Production
Integrated high-speed palletizing and end-of-line systems engineered to keep pace with continuous production. From product infeed and layer formation to pallet supply, palletizing and finished pallet handling, each process is designed around the required line output.
HIGH-OUTPUT HANDLING
SYSTEM ARCHITECTURE
SYSTEM ARCHITECTURE
WHEN DOES A LINE NEED A HIGH-SPEED SOLUTION?
Applications with High Output and Continuous Production
A high-speed end-of-line solution becomes important when upstream production must run continuously and downstream handling needs to keep pace without creating unnecessary accumulation or production interruptions.
The required system architecture depends not only on nominal output, but also on the number of incoming lines, product flow, buffering conditions, pallet change and downstream handling.
High Upstream Output
Production output requires downstream handling to process products without restricting the upstream line.
OUTPUT · LINE CAPACITY
Continuous Production
Long or continuous production runs require stable product flow and coordinated downstream equipment.
CONTINUOUS · STABLE FLOW
Multiple Infeed Lines
Products arriving from two or more upstream lanes may require distribution, merging or parallel palletizing.
SINGLE · DUAL · MULTI-INFEED
Limited Buffering Time
When accumulation space is limited, downstream processes must respond quickly to changes in product flow.
BUFFER · ACCUMULATION
Fast Pallet Change
Empty pallet supply and completed pallet transfer should be coordinated with palletizing to reduce unnecessary production interruptions.
PALLET SUPPLY · CHANGEOVER
Downstream Bottlenecks
Palletizing, pallet transport or other downstream processes can limit overall line performance if they are not balanced with upstream production.
PALLETIZING · OUTFLOW
When should a high-speed palletizing system be considered?
A high-speed palletizing system should be evaluated when downstream handling must continuously match high upstream output, multiple infeed lines or limited buffering conditions. The complete product and pallet flow should be considered together rather than selecting the palletizer by speed alone.
WHERE DOES THE BOTTLENECK USUALLY OCCUR?
A Line Is Only as Fast as Its Weakest Process
In a high-speed production line, overall output depends on the complete downstream flow—not only on the nominal speed of the palletizing machine.
Product infeed, distribution, grouping, palletizing, pallet change and finished pallet handling must work together. If one process cannot keep pace, accumulation or production interruptions may occur upstream.
01
→
Product Infeed
Stable incoming product flow
02
→
Product Distribution
Lane balancing and accumulation
03
→
Row / Layer Formation
Product grouping and arrangement
04
→
Automatic Palletizing
Coordinated product placement
05
→
Finished Pallet Outfeed
Empty pallet replacement
06
Full Pallet Outfeed
Finished pallet transfer
What usually limits the output of a high-speed palletizing line?
The bottleneck may occur at product infeed, distribution, layer formation, palletizing, pallet change or finished pallet transfer. For this reason, high-speed line capacity should be evaluated as a complete material-flow system rather than by palletizer speed alone.
HOW A HIGH-SPEED PALLETIZING LINE WORKS
From High-Speed Infeed to Finished Pallet
A high-speed end-of-line system coordinates product handling, product distribution, palletizing and pallet flow to maintain continuous production from upstream infeed to finished pallet outfeed.
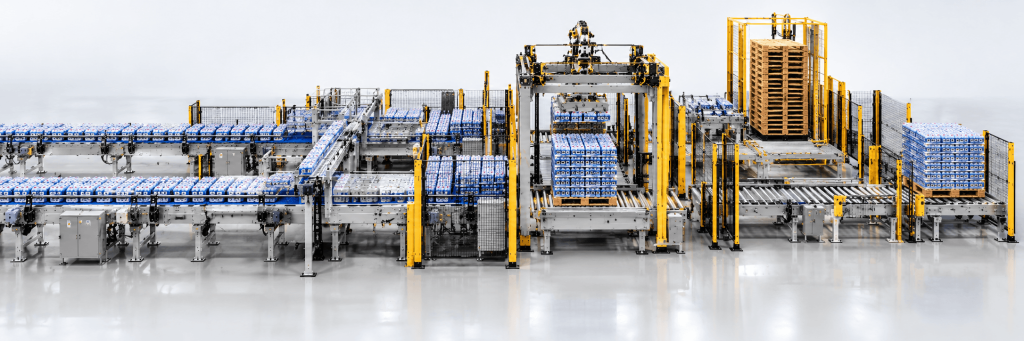
01 —
High-Speed Infeed
Products enter from one or multiple upstream production lines in a controlled and continuous flow.
SINGLE / MULTI-INFEED
02 —
Product Distribution
Products are divided, aligned or accumulated according to the required downstream handling sequence.
DIVIDE · ALIGN · BUFFER
03 —
Row / Layer Formation
Products are grouped into the required row or complete-layer arrangement before palletizing.
GROUP · ARRANGE · FORM
04 —
Automatic Palletizing
Prepared products are transferred onto the pallet using the selected high-speed palletizing configuration.
HANDLE · PLACE · STACK
05—
Automatic Pallet Supply
Empty pallets are automatically supplied and transferred into the palletizing position for continuous operation.
SUPPLY · TRANSFER
06 —
Full Pallet Outfeed
Completed pallet loads are transferred downstream for wrapping, storage or further logistics handling.
OUTFEED · WRAPPING · LOGISTICS
CONTINUOUS FLOW MATTERS
In high-speed applications, product handling and pallet handling operate as one coordinated system. Pallet supply, product accumulation and finished pallet transfer should be designed to prevent unnecessary stops during continuous production.
HIGH-SPEED SYSTEM CONFIGURATIONS
Different Architectures for Different Production Requirements
High-speed palletizing does not rely on one fixed machine configuration. The suitable architecture should be selected around the required output, number of incoming lines, product format, pallet pattern and overall production flow.
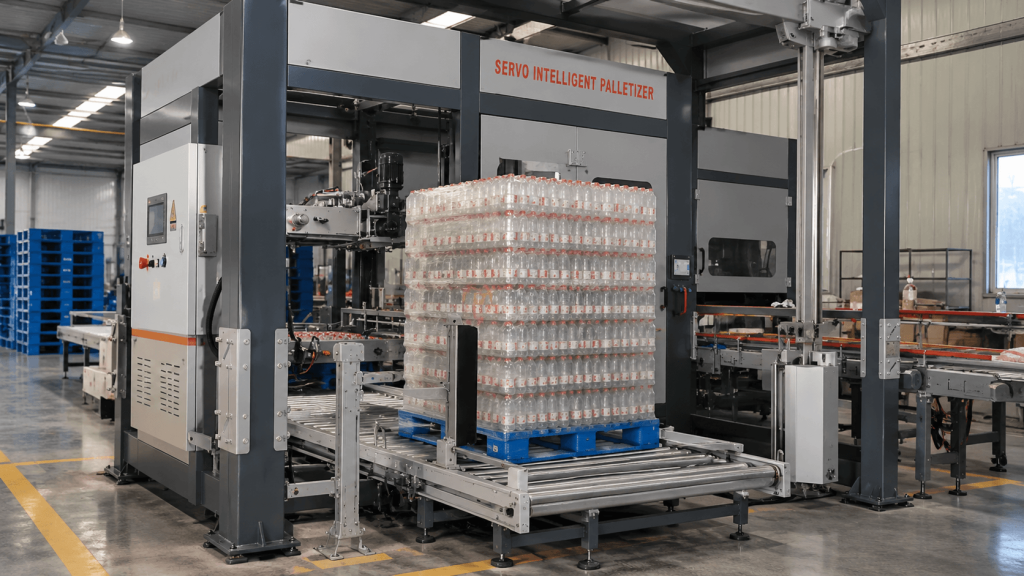
SINGLE-LANE SYSTEM
Single-Lane High-Speed Palletizing
A compact high-output configuration for production lines where products arrive through one primary infeed and can be continuously organized for palletizing.
Best evaluated when:
- One primary product infeed
- Stable and continuous production
- Repeatable product and pallet patterns
- Compact system architecture is preferred
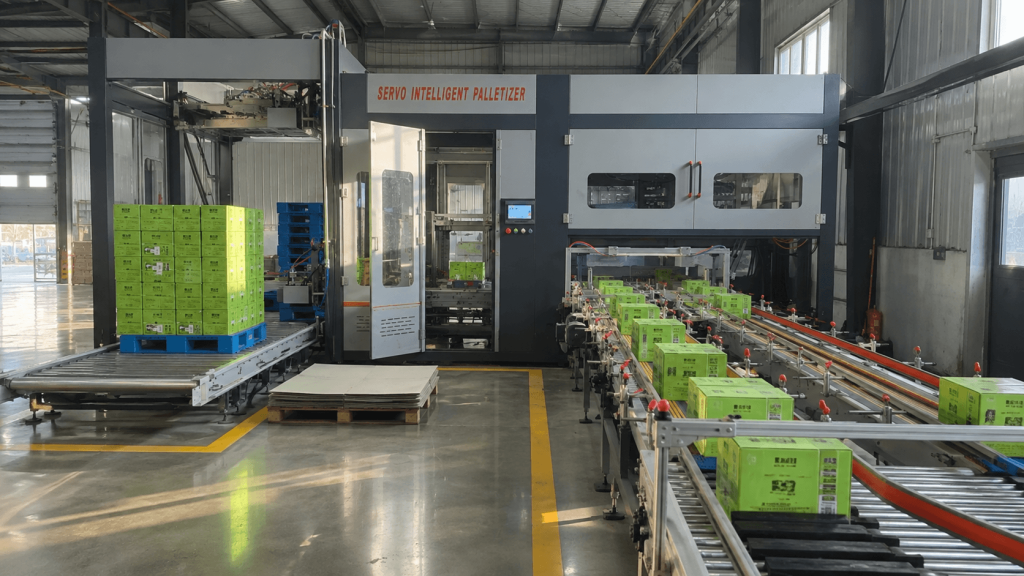
DUAL-LANE / DUAL-CHANNEL
Dual-Channel High-Speed Palletizing
A parallel handling architecture for applications where two product streams or coordinated handling paths are used to support continuous high-output production.
Best evaluated when:
- Two incoming product lanes
- Higher combined production output
- Parallel product handling is required
- Palletizing and pallet flow must remain synchronized
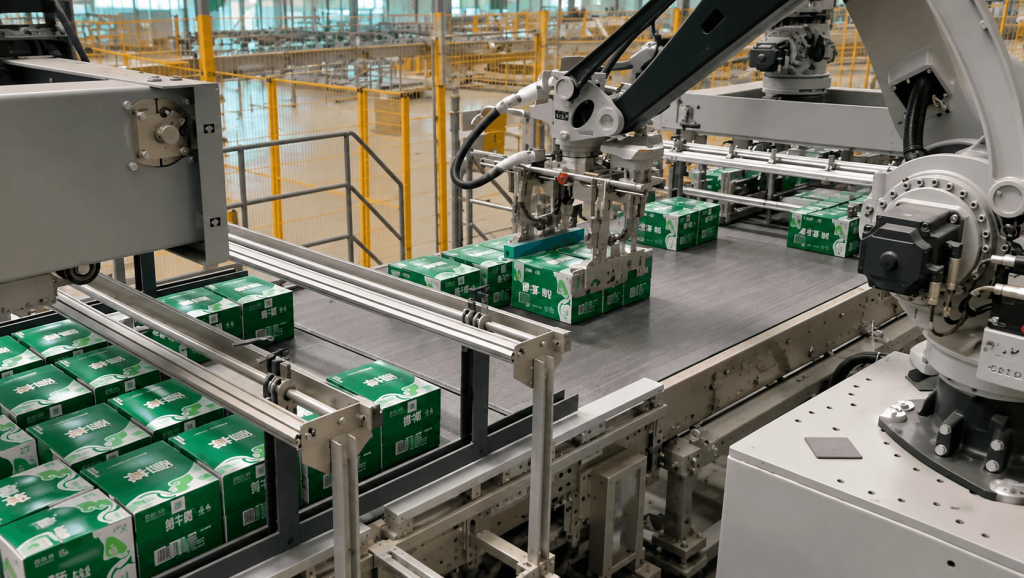
MULTI-INFEED ROBOTIC
Multi-Infeed Robotic Palletizing
A flexible robotic architecture for applications requiring products from multiple infeed lines to be grouped, coordinated and palletized within one integrated system.
Best evaluated when:
- Multiple product infeed lines
- Flexible grouping or handling is required
- Product formats or pallet patterns may vary
- Robotic handling fits the required line architecture
HOW DO WE SELECT THE RIGHT ARCHITECTURE?
The Production Flow Should Be Evaluated as a Complete System
The required output is only one part of the selection process. Infeed configuration, product format, grouping method, pallet change, downstream handling and available site conditions should be evaluated together.
WHY HEIGHT MATTERS
More height, fewer pallets, lower freight cost
Standard palletizers typically stack to 1,200–1,500mm. ATOP high-level systems stack up to 2,000mm — meaning more product per pallet, fewer pallets per shipment, and lower outbound freight cost per unit shipped.
ENGINEERED FOR LINE BALANCE
More Than a Fast Machine — A Balanced Production Line
The fastest machine does not necessarily create the fastest production line. A high-speed system should be engineered around the complete flow of products and pallets, from upstream output and product distribution to pallet change and downstream handling.
The goal is to keep each process coordinated so that one section of the line does not create unnecessary accumulation, waiting time or production interruptions elsewhere.
01
Upstream Production Output
Actual production rate, peak output and production stability define how much downstream handling capacity is required.
OUTPUT · PEAK RATE · STABILITY
02
Number of Infeed Lines
Single, dual or multiple incoming product lanes affect product distribution, accumulation and system architecture.
SINGLE · DUAL · MULTI-INFEED
03
Product & Pack Format
Product dimensions, pack arrangement and handling characteristics influence grouping, layer formation and palletizing.
SIZE · ARRANGEMENT · HANDLING
04
Accumulation & Buffering
Proper accumulation can help absorb short variations between upstream production and downstream palletizing processes.
BUFFER · ACCUMULATION · FLOW
05
Pallet Supply & Change
Empty pallet supply and completed pallet transfer should be coordinated with the palletizing cycle to minimize unnecessary interruptions.
SUPPLY · CHANGE · TRANSFER
06
Downstream Pallet Flow
Finished pallets should leave the palletizing area efficiently and connect with wrapping, storage or further logistics handling as required.
OUTFLOW · WRAPPING · LOGISTICS
Why is line balancing important in high-speed palletizing?
Line balancing helps coordinate upstream production, product handling, palletizing, pallet change and downstream pallet flow. If one process consistently operates below the required line demand, it can create accumulation or interruptions even when the palletizer itself has sufficient capacity.
REAL HIGH-SPEED ATOP PROJECTS
High-Output Palletizing in Real Production Lines
Different production lines require different system architectures. These ATOP projects show how high-output applications can be engineered around actual product flow, infeed configuration, palletizing requirements and downstream handling.
DUAL-CHANNEL PALLETIZING
70,000 BPH Dual-Channel Palletizing Line
A high-output dual-channel palletizing system engineered to handle continuous production through coordinated product flow, palletizing and finished pallet transfer.
PROJECT FLOW
Product Infeed → Layer Formation → Dual-Channel Palletizing → Full Pallet Outfeed → Stretch Wrapping
HIGH-SPEED PALLETIZING
36,000 BPH Palletizing Line
A continuous high-speed palletizing application integrating product handling, palletizing and downstream pallet flow.
OUTPUT
36,000 BPH
CONFIGURATION
Single-Line / Single-Channel
DOWNSTREAM
Stretch Wrapping
DUAL-INFEED ROBOTIC PALLETIZING
80,000 BPH Dual-Infeed Robotic System
A high-output robotic palletizing configuration using coordinated product infeed and grouped handling to support continuous production.
OUTPUT
80,000 BPH
INFEED
Dual-Infeed
PALLETIZING
Robotic Group Handling
DIFFERENT OUTPUT. DIFFERENT ARCHITECTURE.
High-speed palletizing should be engineered around the actual production line rather than a fixed machine specification. Product format, infeed configuration, pallet pattern and downstream flow can all affect the final system design.
FREQUENTLY ASKED QUESTIONS
Common Questions About High-Speed Palletizing Lines
High-speed applications involve more than palletizer capacity alone. Infeed configuration, product flow, pallet change, downstream handling and existing line conditions should all be considered when defining the system.
Have a high-output production line?
What determines the capacity of a high-speed palletizing line?
The achievable line capacity depends on the product format, incoming product flow, number of infeed lanes, grouping or layer-formation process, palletizing method, pallet change and downstream pallet handling. For this reason, capacity should be evaluated across the complete system rather than by palletizer speed alone.
When should a dual-channel palletizing system be considered?
A dual-channel configuration can be considered when two product streams need to be handled in parallel or when the required production flow benefits from coordinated parallel processing. The final architecture should be determined according to actual output, infeed conditions, product format and pallet requirements.
Can one palletizing system receive products from multiple production lines?
Yes, depending on the application. Products from multiple infeed lines can be distributed, accumulated or grouped before palletizing, but the required architecture depends on product format, line output, pallet patterns and how the incoming flows need to be coordinated.
How is pallet change handled during high-speed production?
Empty pallet supply and finished pallet transfer can be integrated with the palletizing process to reduce unnecessary interruptions. The pallet-handling sequence should be designed around the palletizing cycle, required output and available accumulation capacity.
Can a high-speed palletizing system integrate with an existing production line?
Yes. The system can be engineered around existing upstream and downstream equipment. Product discharge conditions, conveyor height, infeed direction, available floor space, control interfaces and downstream pallet flow should be reviewed before the final layout is defined.
What information is needed to design a high-speed palletizing system?
Start with the product or package format, current and target output, number of infeed lines, pallet dimensions, required pallet pattern and information about the existing production line. Photos, videos and a layout drawing are also useful for the initial evaluation.
If complete technical data is not yet available, a short production-line video and basic product information are enough to begin the discussion.
START YOUR HIGH-SPEED PROJECT
Planning a High-Output Production Line?
Tell us what you are producing, your current or target output and how products arrive at the end of the line. Our team can evaluate the suitable palletizing architecture and overall product and pallet flow around your production requirements.
You do not need a complete technical specification to begin.